 Show me a washed-out, gray-looking white print on a black tee and I can usually name the culprit before the shirt even comes off the platen. It isn’t the print head. It isn’t the RIP profile. Nine times out of ten it’s the invisible step that happened before the garment ever saw a drop of ink.
Here’s the uncomfortable truth the DTG world likes to dance around: on a dark garment, pretreatment isn’t a supporting actor. It is the print. The white ink you lay down is only as good as the chemistry sitting underneath it, and no amount of premium hardware will rescue a shirt that was prepped badly.
Why White Ink Is a Div
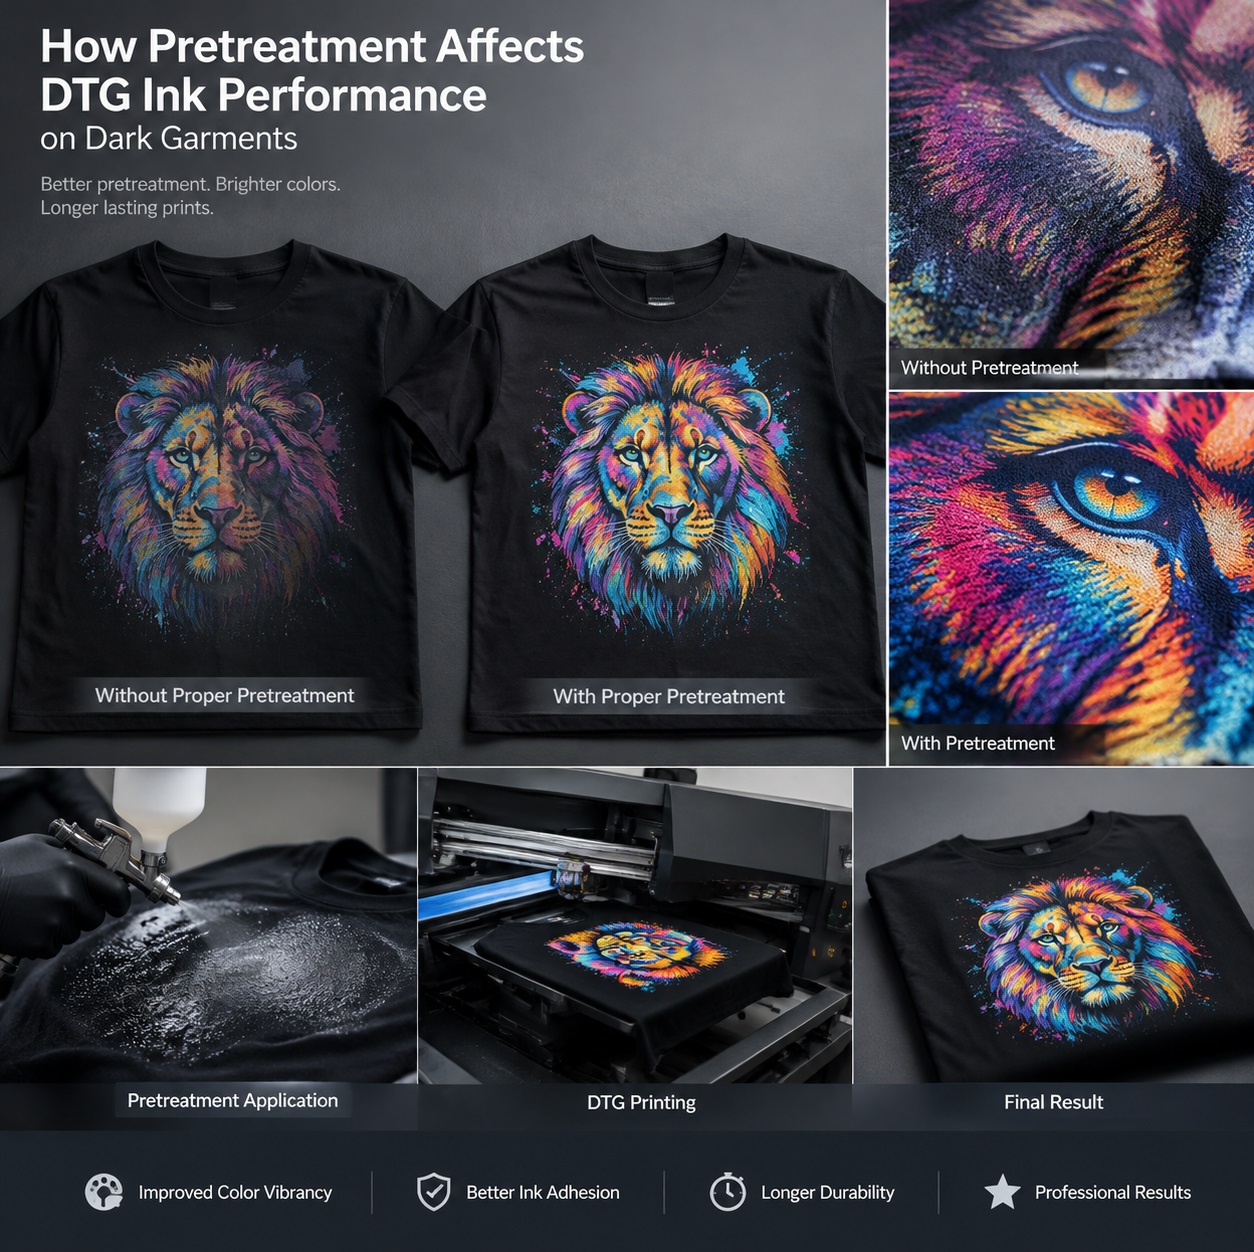
Start with what white ink actually is. It’s pigment particles suspended in a carrier liquid, and those particles are heavy. Spray them onto raw cotton and the fabric does what cotton is designed to do: it drinks. The carrier wicks down into the fiber, dragging pigment with it, and what’s left on the surface is a thin, translucent film that looks gray on black and almost invisible on navy.
That’s the entire battle. You are trying to keep pigment parked on the surface of a material that has spent its whole existence absorbing liquids.
What Pretreatment Actually Does
A good pretreatment solution is doing four jobs at once, and it’s worth naming them because most operators only think about the first one.
It coagulates the pigment. The solution carries cationic polymers that grab the negatively charged pigment particles the moment they land. The ink drops stop dead instead of soaking in. That’s your opacity.
It levels the fabric. Cotton jersey is a landscape of peaks and valleys. Pretreat fills the valleys and lays the fibers down flat, which is why a pretreated shirt prints smooth instead of showing every thread through the white.
It anchors the print. The pretreatment chemistry crosslinks with the pigment binder during curing, which is what separates a print that survives fifty washes from one that starts cracking at twenty.
It controls dot gain. Ink that spreads is ink that blurs. When the surface is properly sealed, halftones stay halftones, fine type stays legible, and edges stay sharp instead of feathering into a halo.
Miss any one of those and the symptom shows up in a different place. That’s what makes pretreatment so frustrating to troubleshoot: the problem and the cause rarely live in the same room.
The Cost of Going Light
Under-pretreated garments fail in a very specific, very recognizable way. The white looks dingy and slightly translucent. Colors printed on top of it lose their punch because the underbase is dragging them down. The print feels thin when you run a thumb across it.
Then you wash it. Cracking appears along the grain of the fabric, corners lift, and the whole design fades two shades. The customer blames the ink. The ink was fine.
The Cost of Going Heavy
Over-pretreatment is the more common mistake in shops that just upgraded their sprayer and haven’t recalibrated. Too much solution and you get a stiff, cardboard hand that customers notice immediately. On lighter darks you’ll see a visible rectangle of discoloration around the print area. Whites can scorch and yellow during curing. Worst of all, excess moisture left in the shirt can cause the white ink to blister or fail to cure properly, which is a durability problem no wash test will forgive.
More is not better. Correct is better.
Uniformity Beats Volume
Here’s the part that separates professional shops from hobby setups. The number of grams you spray matters far less than how evenly you spray it.
An uneven application produces a mottled white, patchy opacity, and inconsistent hand feel across a single shirt. Two shirts from the same run can look like they came from different shops. If your operator’s spray pattern has a hot spot in the middle, you’ll see it in every print, forever.
Most shops land somewhere between 15 and 30 grams for an average adult tee. That number should be written down, measured, and repeated. If it lives in someone’s wrist, it isn’t a process. It’s a guess.
Drying Is Not Optional
Wet pretreatment and DTG ink do not coexist. If you print onto a damp shirt, the ink sits on a film of liquid, the print smears, and you contaminate the platen and potentially the head path.
Dry it properly. Heat press or conveyor, consistent temperature, consistent dwell, and let the garment cool and stabilize before it goes on the platen. A shirt that’s still warm and steaming will give you a different result than one at room temperature, and that variance will show up in your white opacity.
Match the Chemistry to the Fabric
A 100% ring-spun cotton tee and a 50/50 poly blend are not the same substrate, and they don’t want the same pretreatment. Poly needs a different formulation, often with lower water content, because synthetic fibers don’t absorb the same way and dye migration becomes a real threat. Reds, royals, and navy blues are notorious for bleeding into white ink during curing, and the right pretreatment paired with a proper low-cure protocol is your only real defense.
Keep a log of garment brand, style, fabric content, and dye lot. When a run goes sideways, that log is the only thing that will tell you whether the problem is your process or your blanks.
The Variables Nobody Writes Down
Humidity in the shop. How long pretreated shirts sit on the rack before printing. Whether the solution was mixed with tap water that changed chemistry last month. Whether the spray nozzle got cleaned this week.
These are the things that turn a reliable process into a coin flip. None of them are glamorous. All of them show up in the final print.
The Takeaway
On dark garments, pretreatment is where your print quality is decided. Not at the print head, not in the color profile, not in the curing oven. By the time ink hits the shirt, the outcome is mostly locked in.
Invest in the unglamorous part. Calibrate your spray volume. Train on uniformity. Control your drying. Log your variables. Do that and your white ink will finally start performing the way the spec sheet promised, on every shirt, every run, every time.